Electronics Sourcing
Dual-Sourcing RC Toy Electronics Without Version Drift
Dual sourcing can protect continuity, but only when both electronic paths are qualified as part of the complete toy rather than compared as loose components.
Direct answer: Define a controlled approved-parts list, test each electronics route in the finished vehicle and keep version identity visible through production and after-sales. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Sourcing Checklist: What to Confirm Before You Place an Order, What Should Buyers Check for Toy Type and Age Group When Sourcing Remote Control Toys?, What Should Buyers Check for Speed and Motor When Sourcing Remote Control Toys?.
1. Define the real equivalence target
Compare the behavior a user and inspector can observe, not merely connector shape and nominal voltage.
A replacement board may fit the chassis but respond differently to steering input, low battery state or pairing. Set acceptance criteria for drive, steering, radio coexistence, heat, shutdown and any light or sound function. The target is the approved customer experience for the same SKU. Where a difference is commercially meaningful, treat it as a new variant rather than forcing an equivalence claim.
During factory testing and shipment preparation, use define the real equivalence target as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Control controller pairing
Verify every approved transmitter and receiver combination under realistic first-use conditions.
A sample may pair in a quiet lab but confuse consumers after a battery change or when several vehicles are nearby. Test the setup sequence from the printed instructions, including recovery after power loss. Record firmware versions where relevant. Replacement controllers for service stock should be matched to the correct electronics revision instead of being marketed as universally compatible.
During factory testing and shipment preparation, use control controller pairing as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Review mechanical and electrical fit
Check mounting, wire routing, connector retention, current draw and space around moving parts.
A substitute board may put a connector closer to a wheel, need a different screw or heat a nearby plastic feature. Build both versions into representative finished vehicles. Inspect after routine driving and handling, not only after a bench power-on. Keep engineering drawings and the exact sample IDs in the qualification record so production can repeat the approved build.
During factory testing and shipment preparation, use review mechanical and electrical fit as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Reassess regulatory evidence
Ask qualified radio and toy-compliance advisers which tests or files need updating after the change.
A different radio module, antenna layout or firmware may affect the evidence behind market approval. A supplier statement that both parts use 2.4 GHz is not a compliance assessment. Keep reports tied to the actual hardware and firmware. If the alternate cannot be documented before the shipping deadline, delay or separate it rather than mixing uncertain units into an approved batch.
During factory testing and shipment preparation, use reassess regulatory evidence as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Set production changeover rules
Define when each approved route may be used and how lots will be identified.
Avoid changing boards halfway through a carton without a traceable boundary. Factory records should show component supplier, revision, line date and finished-product lot. The buyer may accept either route, but customer support needs to know which one shipped. A simple visible code can make future service and complaint analysis much more reliable.
During factory testing and shipment preparation, use set production changeover rules as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Compare supply economics
Include qualification, inspection and service inventory costs in the dual-source decision.
A cheaper board is not necessarily cheaper once test work, tooling changes, separate spare controllers and more complex warranty handling are included. Build a volume model for both routes and the value of continuity. Some programs justify a second source only for high-risk components. Others are better served by a safety stock of the existing approved part.
During factory testing and shipment preparation, use compare supply economics as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Keep the alternate ready
Run periodic confirmation builds rather than leaving the backup supplier untested for a year.
Components and firmware can change while an alternate sits idle. A short planned run helps verify current materials, drawings, test files and capacity. Do not assume a past sample approval covers every future lot. Update the approved-parts list whenever a change is made, and keep the buyer’s signed decision with the project file.
During factory testing and shipment preparation, use keep the alternate ready as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A distributor wants a backup receiver board because the current component has an uncertain lead time. Two boards appear interchangeable on a workbench, and both respond to the same transmitter during a short test. A complete qualification trial reveals that the alternate board pairs differently after power is interrupted and places a wire near the steering linkage. The engineering team reroutes the wire, updates the pairing instruction and asks the relevant compliance specialist to review the radio evidence. The buyer must then decide whether both boards can share a retail SKU or whether the changed user sequence requires a distinct version. Production records map board supplier to finished lot, while service staff receive a compatibility table for replacement remotes. This is a resilience strategy only after the alternate route has been approved in the complete toy; before that, it is a proposed substitution.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISO quality management guidance on external providers: Official ISO auditing guidance on controlling externally provided products and services.
Photography plan for this article
Article hero image — After the opening section
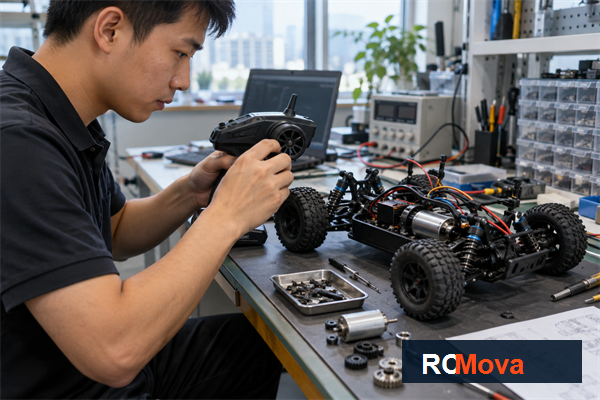
Image title: Dual-Sourcing RC Toy Electronics Without Version Drift — RC toy sourcing overview
Caption: Controller selection should be tested as part of the complete vehicle and user experience. Article focus: dual source rc toy electronics.
ALT text: Asian electronics technician testing an RC controller and vehicle components; dual source rc toy electronics buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for Dual-Sourcing RC Toy Electronics Without Version Drift, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
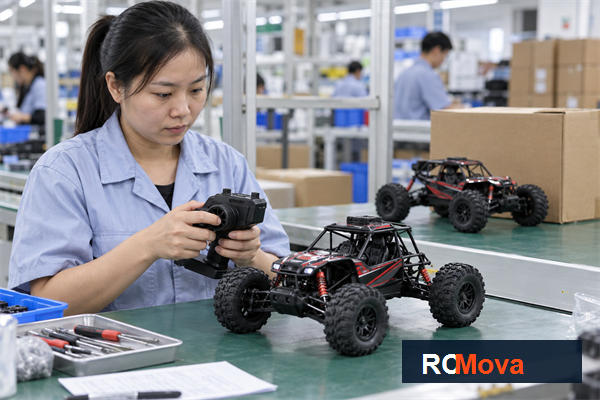
Image title: Dual-Sourcing RC Toy Electronics Without Version Drift — RC toy quality and shipment check
Caption: Production review for dual source rc toy electronics before the export handoff.
ALT text: Asian quality team reviewing dual source rc toy electronics with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking dual source rc toy electronics against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about define the real equivalence target?
Compare the behavior a user and inspector can observe, not merely connector shape and nominal voltage. A replacement board may fit the chassis but respond differently to steering input, low battery state or pairing. Set acceptance criteria for drive, steering, radio coexistence, heat, shutdown and any light or sound function. The target is the approved customer experience for the same SKU. Where a difference is commercially meaningful, treat it as a new variant rather than forcing an equivalence claim.
How should buyers verify reassess regulatory evidence?
Ask qualified radio and toy-compliance advisers which tests or files need updating after the change. A different radio module, antenna layout or firmware may affect the evidence behind market approval. A supplier statement that both parts use 2.4 GHz is not a compliance assessment. Keep reports tied to the actual hardware and firmware. If the alternate cannot be documented before the shipping deadline, delay or separate it rather than mixing uncertain units into an approved batch.
What should be confirmed before shipment?
Run periodic confirmation builds rather than leaving the backup supplier untested for a year. Components and firmware can change while an alternate sits idle. A short planned run helps verify current materials, drawings, test files and capacity. Do not assume a past sample approval covers every future lot. Update the approved-parts list whenever a change is made, and keep the buyer’s signed decision with the project file.
Conclusion: turn the decision into a working plan
Define a controlled approved-parts list, test each electronics route in the finished vehicle and keep version identity visible through production and after-sales. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements