Battery Quality
RC Toy Battery Capacity and Pack Consistency Checks
Battery quality for an RC toy should be evaluated through controlled pack identity, supplier evidence, sampled electrical checks and representative finished-product use. Results must be tied to the exact cell, protection circuit, connector and charging arrangement.
Direct answer: Approve the complete battery pack specification, trace production lots and verify capacity-related behavior using defined conditions before relying on runtime or charging claims. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Buyers need to understand and control battery variation that affects runtime, charging experience, power delivery and customer complaints. A nominal label does not by itself demonstrate usable capacity, protection behavior or lot consistency in the finished toy.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Battery Shipping Guide: What Buyers Should Confirm Before Dispatch, What Should Buyers Check for Battery and Charging When Sourcing Remote Control Toys?, What Should Buyers Check for Battery and Charging When Sourcing RC Toys?.
1. Define the complete pack
Specify cell chemistry, configuration, nominal data, protection, connector, wire, enclosure, charger compatibility and approved supplier.
Capacity cannot be separated from the finished pack and charging method. Link labels and transport records to the same configuration. Treat a cell or protection-board change as a controlled product change.
During factory testing and shipment preparation, use define the complete pack as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Maintain lot traceability
Record battery supplier batch, factory receipt, production use and affected finished-toy lots.
Traceability supports containment when runtime, charging or physical-condition concerns appear. Keep mixed batches separated where practical. Carton or product records should allow a reasonable investigation without exposing unnecessary consumer data.
During factory testing and shipment preparation, use maintain lot traceability as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Inspect condition at receipt
Check packaging, pack dimensions, leads, connectors, markings and signs of damage or contamination.
Do not use swollen, leaking, crushed or otherwise suspicious packs. Follow qualified battery-handling procedures for isolation and disposition. Visual checks cannot establish capacity but can prevent obviously damaged material from entering production.
During factory testing and shipment preparation, use inspect condition at receipt as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Use controlled electrical sampling
Define equipment, charge method, rest time, discharge conditions, temperature and acceptance approach with qualified engineers.
Capacity results vary with the method. Compare like-for-like lots and retain raw records. Avoid promising that limited internal sampling replaces required safety, transport or compliance testing.
During factory testing and shipment preparation, use use controlled electrical sampling as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Confirm finished-toy behavior
Use the approved vehicle, surface and operating routine to observe runtime, power delivery and low-voltage behavior.
Drivetrain friction, driver pattern and battery state influence the result. State conditions with any performance claim. Compare several representative units rather than one best sample.
During factory testing and shipment preparation, use confirm finished-toy behavior as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Control storage and rotation
Set appropriate conditions, inventory age, state-of-charge practices and first-in-first-out use with battery specialists.
Long storage can change the customer experience. Recheck older stock before shipment when risk warrants it. Keep terminals protected and avoid uncontrolled charging in storage areas.
During factory testing and shipment preparation, use control storage and rotation as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Escalate variation and changes
Investigate unusual spread, early cutoff, heat, swelling or charging differences before release.
Contain affected lots and review the pack, charger and vehicle system together. Document supplier corrective action and repeat relevant checks after any component or process change.
During factory testing and shipment preparation, use escalate variation and changes as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
Two batches of the same RC crawler use packs with the same printed capacity, but one produces noticeably shorter runtime. The factory’s function test confirms movement but does not measure pack variation. In this illustrative scenario, the buyer and supplier define lot sampling, controlled charge-discharge observations and a finished-vehicle runtime screen for engineering review. The decision focuses on consistent customer experience without presenting a small factory sample as laboratory certification.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see IATA 2026 lithium battery guidance document: Current IATA guidance on classification, state of charge, packing, marking and air-transport responsibilities.
Photography plan for this article
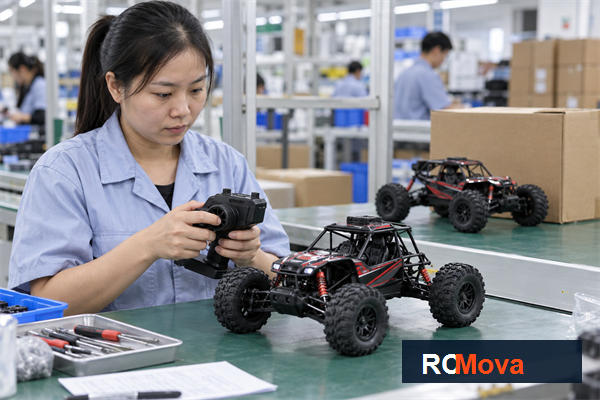
Article hero image — After the opening section
Image title: RC Toy Battery Capacity and Pack Consistency Checks — RC toy sourcing overview
Caption: Function checks and inspection records help keep an approved configuration consistent before packing. Article focus: rc toy battery capacity test.
ALT text: Asian quality inspector testing an RC vehicle at a Shenzhen factory inspection bench; rc toy battery capacity test buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Battery Capacity and Pack Consistency Checks, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
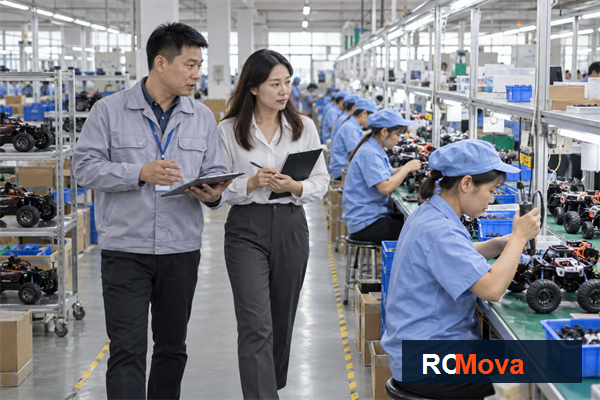
In-article supporting image — Before the FAQ section
Image title: RC Toy Battery Capacity and Pack Consistency Checks — RC toy quality and shipment check
Caption: Production review for rc toy battery capacity test before the export handoff.
ALT text: Asian quality team reviewing rc toy battery capacity test with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy battery capacity test against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about define the complete pack?
Specify cell chemistry, configuration, nominal data, protection, connector, wire, enclosure, charger compatibility and approved supplier. Capacity cannot be separated from the finished pack and charging method. Link labels and transport records to the same configuration. Treat a cell or protection-board change as a controlled product change.
How should buyers verify use controlled electrical sampling?
Define equipment, charge method, rest time, discharge conditions, temperature and acceptance approach with qualified engineers. Capacity results vary with the method. Compare like-for-like lots and retain raw records. Avoid promising that limited internal sampling replaces required safety, transport or compliance testing.
What should be confirmed before shipment?
Investigate unusual spread, early cutoff, heat, swelling or charging differences before release. Contain affected lots and review the pack, charger and vehicle system together. Document supplier corrective action and repeat relevant checks after any component or process change.
Conclusion: turn the decision into a working plan
Approve the complete battery pack specification, trace production lots and verify capacity-related behavior using defined conditions before relying on runtime or charging claims. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements