Appearance Quality
RC Toy Color Masters and Appearance Standards
A color master is a controlled physical reference for the approved appearance of an RC toy. It helps the factory and buyer evaluate production color under agreed conditions instead of relying on memory or screen images.
Direct answer: Approve color on representative materials and finished parts, define viewing conditions and tolerance handling, and preserve the reference through production and shipment inspection. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Brand and retail buyers need consistent color and finish across plastic, paint, printing and packaging components. Digital files and color codes do not show every material, texture, gloss and viewing-condition effect on a finished RC toy.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see Custom RC Toy Body, Color and Accessories: Buyer Guide, How to Choose an RC Toy Manufacturer for Your Market, RC Toy Sourcing Checklist: What to Confirm Before You Place an Order.
1. Define every visible surface
List molded plastic, painted parts, tires, decals, controller, accessories and packaging that participate in the color story.
A buyer may request blue without specifying whether wheel hubs, controller buttons and carton photography should match exactly or coordinate. Mark each surface on a visual specification. Record material, finish and target reference. This prevents the factory from applying one color instruction to components whose texture and manufacturing process create visibly different results.
During factory testing and shipment preparation, use define every visible surface as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Approve physical material samples
Evaluate color on the intended resin, coating, ink and substrate before releasing bulk production.
A standard color reference supports communication but cannot predict every combination of pigment, plastic thickness, gloss and undercoat. Review representative plaques, decorated parts or a complete sample. If recycled content or a new supplier is introduced, confirm whether the base material changes appearance. Keep screen images for orientation only, not final acceptance.
During factory testing and shipment preparation, use approve physical material samples as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Set practical viewing conditions
Agree light source, distance, angle and comparison method for appearance decisions.
Metamerism can make two colors appear similar under one light and different under another. A factory and buyer comparing parts in unrelated environments may reach opposite conclusions. Use a consistent neutral background and controlled lighting where practical, then consider the retail environment. Record whether instrumental readings support the visual review and which method governs acceptance.
During factory testing and shipment preparation, use set practical viewing conditions as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Control gloss, texture and coverage
Color approval should include surface character, not only hue.
Gloss variation can make a matching pigment look different. Check paint coverage at edges, flow marks, weld lines, sink areas and color show-through. Define whether minor texture differences are acceptable on hidden or functional surfaces. For translucent or metallic finishes, specify orientation and layer construction because a flat color chip may not represent the finished shell.
During factory testing and shipment preparation, use control gloss, texture and coverage as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Manage master custody and aging
Label, protect and periodically compare the approved reference so it remains usable.
Sunlight, heat, handling and chemical exposure can change a physical sample. Keep one protected master with the factory and one with the buyer when possible, each marked with model and revision. Do not replace a faded master informally. If production is seasonal or transferred, create a documented re-approval using fresh representative parts.
During factory testing and shipment preparation, use manage master custody and aging as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Inspect production variation
Sample across time, cavity, batch and color changeover instead of checking only one early unit.
Injection-molded parts from different cavities or pigment batches may shift. Paint settings can drift during the run. Review units near the start, middle and end, and record any known cavity or batch identity. At shipment inspection, compare representative finished sets with the master under the agreed method while recognizing that a small sample cannot describe every unit.
During factory testing and shipment preparation, use inspect production variation as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Tie marketing assets to the approved finish
Use production-representative photography and qualify color language when screens or lighting can alter perception.
A listing image should not promise a finish that the product cannot consistently deliver. Confirm that renders, samples and finished goods use the same revision. If a supplier changes material or coating, review the visual impact before updating photography or continuing production. Accurate appearance communication reduces returns driven by expectation rather than function.
During factory testing and shipment preparation, use tie marketing assets to the approved finish as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A private-label buyer approves a bright orange body from a photograph. During production, the molded chassis, painted shell and printed carton each appear slightly different, even though all files reference the same color code. The parties compare physical samples under neutral light and decide which differences are intentional material effects and which exceed the approved appearance. A finished vehicle becomes the signed master, with separate reference chips for the molded and painted parts. This illustrative scenario shows why a single digital swatch cannot control gloss, opacity, texture and substrate interaction across a complete RC toy set.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see FTC advertising substantiation guidance: Official U.S. guidance on having a reasonable basis for objective marketing claims.
Photography plan for this article
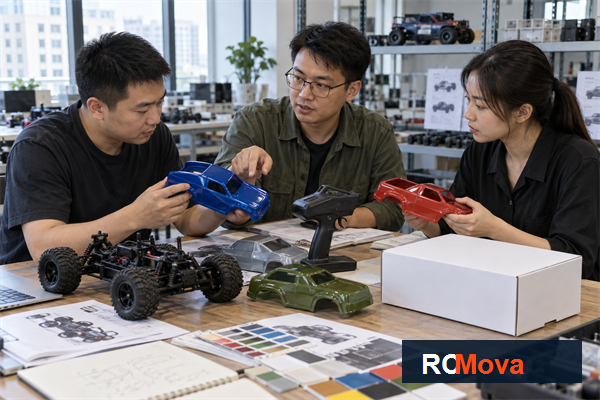
Article hero image — After the opening section
Image title: RC Toy Color Masters and Appearance Standards — RC toy sourcing overview
Caption: An OEM or ODM discussion is clearer when product samples, controllers and packaging direction are reviewed together. Article focus: rc toy color master sample.
ALT text: Asian toy engineers reviewing RC vehicle body shells and packaging samples in Shenzhen; rc toy color master sample buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Color Masters and Appearance Standards, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
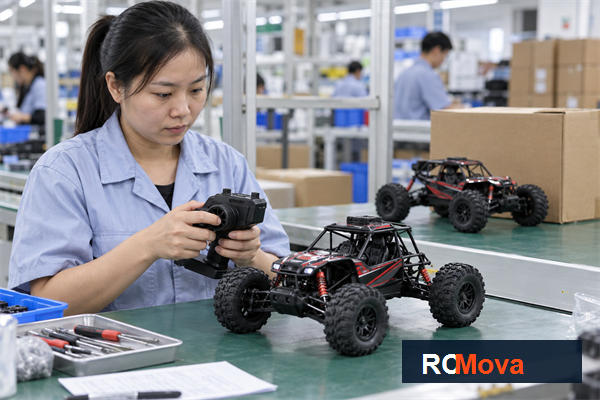
In-article supporting image — Before the FAQ section
Image title: RC Toy Color Masters and Appearance Standards — RC toy quality and shipment check
Caption: Production review for rc toy color master sample before the export handoff.
ALT text: Asian quality team reviewing rc toy color master sample with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy color master sample against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about define every visible surface?
List molded plastic, painted parts, tires, decals, controller, accessories and packaging that participate in the color story. A buyer may request blue without specifying whether wheel hubs, controller buttons and carton photography should match exactly or coordinate. Mark each surface on a visual specification. Record material, finish and target reference. This prevents the factory from applying one color instruction to components whose texture and manufacturing process create visibly different results.
How should buyers verify control gloss, texture and coverage?
Color approval should include surface character, not only hue. Gloss variation can make a matching pigment look different. Check paint coverage at edges, flow marks, weld lines, sink areas and color show-through. Define whether minor texture differences are acceptable on hidden or functional surfaces. For translucent or metallic finishes, specify orientation and layer construction because a flat color chip may not represent the finished shell.
What should be confirmed before shipment?
Use production-representative photography and qualify color language when screens or lighting can alter perception. A listing image should not promise a finish that the product cannot consistently deliver. Confirm that renders, samples and finished goods use the same revision. If a supplier changes material or coating, review the visual impact before updating photography or continuing production. Accurate appearance communication reduces returns driven by expectation rather than function.
Conclusion: turn the decision into a working plan
Approve color on representative materials and finished parts, define viewing conditions and tolerance handling, and preserve the reference through production and shipment inspection. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements