Decoration Quality
RC Toy Paint, Pad Print and Decal Durability
Decoration durability depends on substrate preparation, ink or coating selection, curing, geometry and expected handling. Buyers should approve both appearance and a product-specific verification method.
Direct answer: Identify each decoration process, establish a physical reference and repeatable adhesion or wear check, then monitor production after material and setup changes. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Buyers need decoration that survives packing, handling and foreseeable play without unsupported durability claims. Paint, printed graphics and decals can look correct at approval yet peel, rub or transfer after production conditions change.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see What Should Buyers Check for Durability and Materials When Sourcing Remote Control Toys?, What Should Buyers Check for Durability and Materials When Sourcing RC Toys?, RC Toy Drop Tests and Durability Testing: What Buyers Should Check.
1. Map decoration by process
Identify which graphics are molded color, paint, pad print, screen print, hot stamp, label or decal.
Different processes fail in different ways and require different controls. Mark the artwork location, substrate, finish and supplier on the specification. Clarify whether graphics are functional markings or decorative only. A controller direction symbol deserves closer legibility control than a small body accent because its loss can affect first-use understanding.
During factory testing and shipment preparation, use map decoration by process as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Approve the prepared substrate
Surface material, texture, release residue and cleaning can determine adhesion before ink is applied.
A coating that works on one plastic grade may behave differently after resin, mold release or supplier changes. Review the exact molded part and preparation sequence. Avoid prescribing chemicals without competent technical review. The buyer should ask how the process is controlled and whether the decoration supplier has verified compatibility with the intended substrate.
During factory testing and shipment preparation, use approve the prepared substrate as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Define appearance acceptance
Use a physical master and close-up photographs to control position, coverage, registration and finish.
Set practical expectations for small gaps, edge alignment, dust, pinholes and color variation by visible area. Review curved and recessed zones where printing is difficult. The criterion should match retail viewing and product positioning without demanding an unrealistic cosmetic standard that drives hidden rework or sorting. Document known design limitations before bulk output.
During factory testing and shipment preparation, use define appearance acceptance as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Choose a representative durability check
Match the test to foreseeable rubbing, flexing, contact, moisture or packing pressure.
A tape pull, controlled rub, scratch or conditioning check can provide useful comparative evidence when method, force, material and acceptance are defined. One informal fingernail test is not reproducible. The selected check does not prove unlimited lifetime; it confirms performance under stated conditions for the tested production configuration.
During factory testing and shipment preparation, use choose a representative durability check as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Control curing and handling time
Verify when decorated parts are safe to stack, assemble and pack without transfer or damage.
A surface may feel dry before it has developed stable adhesion. Record the minimum process condition recommended for the selected material and validate it in the actual workflow. Use clean trays or separators where contact marks are possible. Production acceleration should not silently reduce cure or conditioning time to recover a schedule.
During factory testing and shipment preparation, use control curing and handling time as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Monitor changeovers and rework
Inspect early pieces after color, artwork, ink, fixture or operator changes.
Registration and coverage can move during setup. Reworked graphics may have double images, solvent effects or surface damage. Define whether a defect can be reprinted or requires part replacement, and repeat the durability check after an approved rework method. Segregate setup scrap so it cannot be packed as sellable product.
During factory testing and shipment preparation, use monitor changeovers and rework as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Inspect after packing and transport preparation
Review decorated parts inside the final insert, ties and retail carton before shipment.
A decoration process can pass at the workbench and still abrade against packaging during vibration or compression. Open representative packed samples after handling or a defined packaging evaluation. At shipment inspection, look for transfer, peeling and contact marks across sampled cartons, and link any recurring position to insert or retention changes.
During factory testing and shipment preparation, use inspect after packing and transport preparation as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A sample RC sports car has crisp door graphics, but early production units show lifting at a curved decal edge after being removed from the tray. The team checks the film, surface cleanliness, application pressure and insert contact point. The tray is relieved, application instructions are revised and finished units are conditioned before a targeted edge check. In this illustrative buyer scenario, the defect is not solved by pressing the decal down before inspection. The product and packaging process are changed so the approved appearance is more likely to remain stable after shipment and customer handling.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see FTC advertising substantiation guidance: Official U.S. guidance on having a reasonable basis for objective marketing claims.
Photography plan for this article
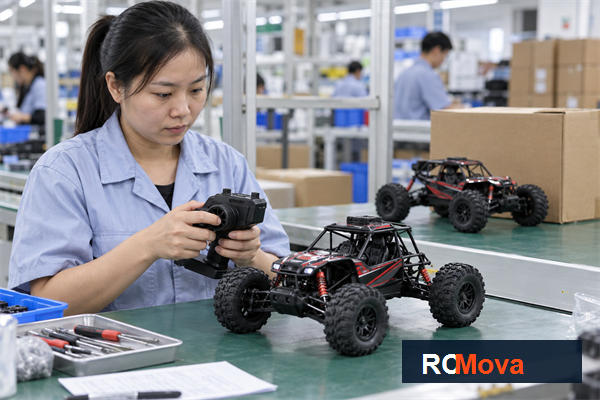
Article hero image — After the opening section
Image title: RC Toy Paint, Pad Print and Decal Durability — RC toy sourcing overview
Caption: Function checks and inspection records help keep an approved configuration consistent before packing. Article focus: rc toy paint adhesion test.
ALT text: Asian quality inspector testing an RC vehicle at a Shenzhen factory inspection bench; rc toy paint adhesion test buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Paint, Pad Print and Decal Durability, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
Image title: RC Toy Paint, Pad Print and Decal Durability — RC toy quality and shipment check
Caption: Production review for rc toy paint adhesion test before the export handoff.
ALT text: Asian quality team reviewing rc toy paint adhesion test with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy paint adhesion test against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about map decoration by process?
Identify which graphics are molded color, paint, pad print, screen print, hot stamp, label or decal. Different processes fail in different ways and require different controls. Mark the artwork location, substrate, finish and supplier on the specification. Clarify whether graphics are functional markings or decorative only. A controller direction symbol deserves closer legibility control than a small body accent because its loss can affect first-use understanding.
How should buyers verify choose a representative durability check?
Match the test to foreseeable rubbing, flexing, contact, moisture or packing pressure. A tape pull, controlled rub, scratch or conditioning check can provide useful comparative evidence when method, force, material and acceptance are defined. One informal fingernail test is not reproducible. The selected check does not prove unlimited lifetime; it confirms performance under stated conditions for the tested production configuration.
What should be confirmed before shipment?
Review decorated parts inside the final insert, ties and retail carton before shipment. A decoration process can pass at the workbench and still abrade against packaging during vibration or compression. Open representative packed samples after handling or a defined packaging evaluation. At shipment inspection, look for transfer, peeling and contact marks across sampled cartons, and link any recurring position to insert or retention changes.
Conclusion: turn the decision into a working plan
Identify each decoration process, establish a physical reference and repeatable adhesion or wear check, then monitor production after material and setup changes. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements