Electronics Process Control
ESD Control for RC Toy Electronics Assembly
ESD control is a process system for protecting susceptible electronic parts during receiving, storage, assembly, inspection, packaging and rework. The necessary controls depend on component sensitivity and the approved manufacturing route.
Direct answer: Ask the electronics provider to define the ESD-sensitive items, protected areas, grounding, packaging, training and verification records relevant to the RC toy assembly. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Buyers auditing electronics assembly want evidence that sensitive boards and components are handled under an appropriate electrostatic-discharge control program. Latent or immediate ESD damage may not be visible during a short finished-product function test.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Quality Control Checklist for B2B Orders, How to Choose a Remote Control System for an RC Toy, How Should Buyers Choose Remote Control Toys?.
1. Identify susceptible items and processes
Map components, boards, subassemblies and handling steps that require ESD protection.
Use supplier data and qualified engineering judgment. Receiving, programming, testing and rework can be as important as final assembly. Do not apply decorative wrist straps as a substitute for a defined control program.
During factory testing and shipment preparation, use identify susceptible items and processes as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Define the protected area
Mark where sensitive items may be opened or handled and which materials, equipment and access rules apply.
The area should reflect the real workflow, including temporary work and maintenance. Keep ordinary plastic, packaging and personal items under appropriate control. Visitors and supervisors need rules as well as operators.
During factory testing and shipment preparation, use define the protected area as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Control grounding and personnel
Use suitable personnel grounding, worksurfaces and equipment connections with verification appropriate to the program.
Methods depend on the task and applicable standard. Records should show that checks occur and failures are addressed. Training must explain why the controls matter and what to do when equipment is unavailable.
During factory testing and shipment preparation, use control grounding and personnel as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Use protective packaging
Keep sensitive parts in suitable protective containers during storage and movement outside the controlled area.
Ordinary bags or foam may generate or hold charge. Packaging selection should follow device sensitivity and handling route. Close and identify containers rather than carrying exposed boards between stations.
During factory testing and shipment preparation, use use protective packaging as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Verify the environment and tools
Assess ionization, humidity influence, isolated conductors, soldering tools and test fixtures where relevant.
Humidity alone is not an ESD program. Monitoring and limits require qualified design. Include repair benches and outsourced programming or testing in the process review.
During factory testing and shipment preparation, use verify the environment and tools as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Manage nonconformance and rework
Contain items handled outside the approved controls and decide verification or disposition through engineering review.
A short functional test may not detect latent damage. Investigate the event, affected time window and product lots. Restore the process before normal release and record the corrective action.
During factory testing and shipment preparation, use manage nonconformance and rework as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Audit implementation, not decoration
Compare written procedures with operator behavior, equipment status, records and material movement.
Ask staff to demonstrate daily checks and explain an alarm response. Review calibration or verification evidence where applicable. Reassess controls when boards, components, layouts or subcontractors change.
During factory testing and shipment preparation, use audit implementation, not decoration as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
An RC car receiver board works during final test but shows intermittent field failures. ESD is one possible cause among many, yet the assembly area has no documented protected-zone checks or component handling rules. In this illustrative scenario, the factory involves a qualified electronics specialist, reviews component sensitivity and establishes a monitored ESD control plan. Corrective work is based on evidence rather than declaring ESD the cause without analysis.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see IEC 61340-5-1 electrostatic-discharge control: Official IEC overview of administrative and technical requirements for an ESD control program for susceptible electronic devices.
Photography plan for this article
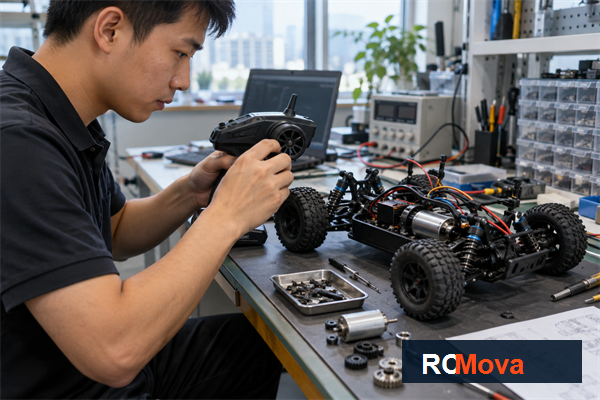
Article hero image — After the opening section
Image title: ESD Control for RC Toy Electronics Assembly — RC toy sourcing overview
Caption: Controller selection should be tested as part of the complete vehicle and user experience. Article focus: rc toy esd control.
ALT text: Asian electronics technician testing an RC controller and vehicle components; rc toy esd control buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for ESD Control for RC Toy Electronics Assembly, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
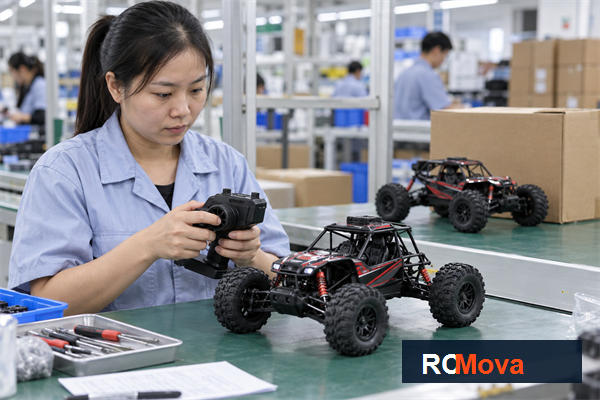
Image title: ESD Control for RC Toy Electronics Assembly — RC toy quality and shipment check
Caption: Production review for rc toy esd control before the export handoff.
ALT text: Asian quality team reviewing rc toy esd control with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy esd control against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about identify susceptible items and processes?
Map components, boards, subassemblies and handling steps that require ESD protection. Use supplier data and qualified engineering judgment. Receiving, programming, testing and rework can be as important as final assembly. Do not apply decorative wrist straps as a substitute for a defined control program.
How should buyers verify use protective packaging?
Keep sensitive parts in suitable protective containers during storage and movement outside the controlled area. Ordinary bags or foam may generate or hold charge. Packaging selection should follow device sensitivity and handling route. Close and identify containers rather than carrying exposed boards between stations.
What should be confirmed before shipment?
Compare written procedures with operator behavior, equipment status, records and material movement. Ask staff to demonstrate daily checks and explain an alarm response. Review calibration or verification evidence where applicable. Reassess controls when boards, components, layouts or subcontractors change.
Conclusion: turn the decision into a working plan
Ask the electronics provider to define the ESD-sensitive items, protected areas, grounding, packaging, training and verification records relevant to the RC toy assembly. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements