Radio & EMC Compliance
EMC Pre-Compliance Planning for RC Toys
EMC pre-compliance is an engineering risk-reduction step performed before formal market testing. It does not create certification, but it can reveal configuration and design problems while changes remain practical.
Direct answer: Freeze a representative configuration, identify applicable market requirements with qualified specialists, screen likely emission and immunity risks, and preserve the exact evidence sent for formal assessment. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Importers and engineering teams want to reduce late laboratory failures before formal radio or EMC assessment. PCB, motor, wiring, enclosure and firmware changes can alter emissions or radio behavior after an early sample has been reviewed.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see Pre-Shipment Inspection for RC Toys: A Buyer’s Practical Guide, ASTM F963 and CPSIA: RC Toy Planning Guide for U.S. Buyers, RC Toy Cartons and Container Loading: Export Planning Guide.
1. Identify the destination requirements
Ask a qualified laboratory or compliance adviser which toy, radio and EMC rules apply to the finished product.
Requirements depend on frequency, transmitter design, market, intended use and economic-operator role. Do not select a test plan from a competitor listing or generic certificate. Provide the vehicle, controller, power arrangement, antennas, firmware and user instructions so the adviser can define the applicable route and sample configuration.
During factory testing and shipment preparation, use identify the destination requirements as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Freeze the electronic baseline
Record PCB revision, motor, suppression parts, wires, battery, controller, antenna and firmware before screening.
Small substitutions can change electrical noise or radio behavior. Photograph the internal layout and mark critical components. If several colors use identical electronics, document that relationship rather than assuming it. A later change should trigger an impact review with the laboratory or responsible technical person before relying on existing evidence.
During factory testing and shipment preparation, use freeze the electronic baseline as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Review likely noise sources
Examine motors, switching circuits, wire loops, contacts and grounding or shielding features that may influence emissions.
Pre-compliance work should be led by competent engineers using suitable equipment. Buyers can still ask how the design controls brush noise, wiring placement and component variation. Avoid decorative metal or conductive coatings changes without review because enclosure and antenna conditions may shift.
During factory testing and shipment preparation, use review likely noise sources as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Screen representative operating modes
Exercise forward, reverse, steering, lights, charging-related states and controller transmission as appropriate.
The highest-risk condition may not be idle. Define battery state, motor load and orientation for repeatability. A screen is useful for comparison and debugging, but its limits and setup should be recorded. Do not advertise a pre-scan as an accredited pass or formal authorization.
During factory testing and shipment preparation, use screen representative operating modes as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Assess coexistence and immunity risks
Consider how the toy behaves around expected radio and electrical environments, not only what it emits.
Observe pairing, loss-of-signal behavior and recovery using the approved configuration. Formal immunity requirements and methods depend on market rules. A showroom multi-vehicle test can support product application, while it remains separate from regulatory assessment. Record unexpected motion or reset behavior for engineering investigation.
During factory testing and shipment preparation, use assess coexistence and immunity risks as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Control the laboratory sample
Send a production-representative, identified unit with accessories, operating instructions and configuration records.
The laboratory needs a way to exercise every relevant mode. Note any special software or cable honestly. Retain a duplicate reference when practical. When a failure drives a modification, update the bill of materials and sample identity, then confirm which tests must be repeated rather than treating an engineering patch as invisible.
During factory testing and shipment preparation, use control the laboratory sample as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Link compliance to production
Protect critical components and layout through purchasing, assembly and change control.
A report describes tested samples; production conformity requires continued control. Define approved alternatives, incoming checks and PCB revision identification. During factory and shipment review, verify model and labeling identity. The importer or responsible party should retain the required technical documentation and seek current market-specific advice.
During factory testing and shipment preparation, use link compliance to production as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
An RC car platform passes an early radio check, then the production design receives a different motor and longer battery wires. A pre-compliance screen shows increased noise near the receiver and reduced control margin in one orientation. Engineering adjusts routing and suppression components, repeats the screen and sends the updated production-representative sample to the accredited test route selected for the market. This illustrative scenario shows why compliance evidence must follow the final electronics configuration; a report for the earlier sample cannot automatically cover every later substitution.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see FCC equipment authorization guidance: Official radio-frequency equipment authorization guidance.
Photography plan for this article
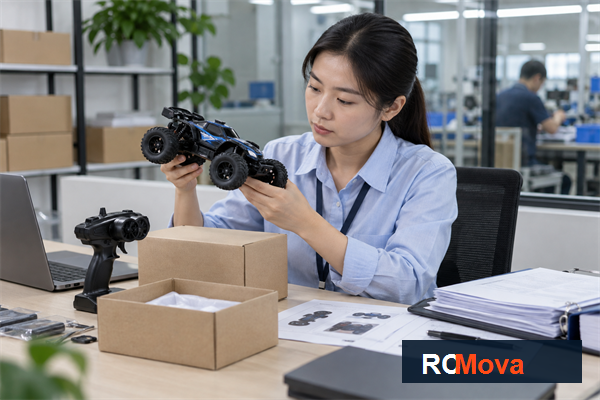
Article hero image — After the opening section
Image title: EMC Pre-Compliance Planning for RC Toys — RC toy sourcing overview
Caption: Compliance preparation should be reviewed against the actual product, packaging and technical records. Article focus: rc toy emc pre compliance.
ALT text: Asian compliance specialist reviewing an RC toy and technical document folder; rc toy emc pre compliance buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for EMC Pre-Compliance Planning for RC Toys, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
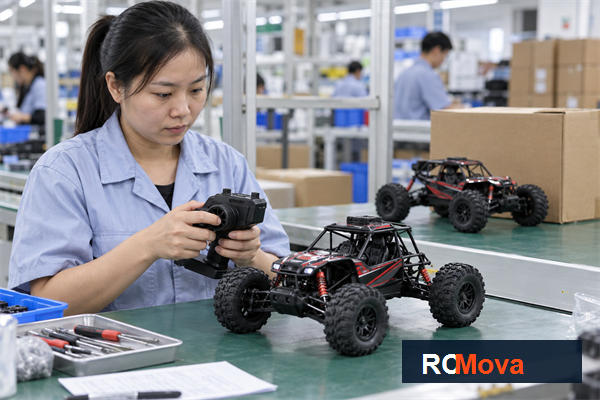
In-article supporting image — Before the FAQ section
Image title: EMC Pre-Compliance Planning for RC Toys — RC toy quality and shipment check
Caption: Production review for rc toy emc pre compliance before the export handoff.
ALT text: Asian quality team reviewing rc toy emc pre compliance with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy emc pre compliance against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about identify the destination requirements?
Ask a qualified laboratory or compliance adviser which toy, radio and EMC rules apply to the finished product. Requirements depend on frequency, transmitter design, market, intended use and economic-operator role. Do not select a test plan from a competitor listing or generic certificate. Provide the vehicle, controller, power arrangement, antennas, firmware and user instructions so the adviser can define the applicable route and sample configuration.
How should buyers verify screen representative operating modes?
Exercise forward, reverse, steering, lights, charging-related states and controller transmission as appropriate. The highest-risk condition may not be idle. Define battery state, motor load and orientation for repeatability. A screen is useful for comparison and debugging, but its limits and setup should be recorded. Do not advertise a pre-scan as an accredited pass or formal authorization.
What should be confirmed before shipment?
Protect critical components and layout through purchasing, assembly and change control. A report describes tested samples; production conformity requires continued control. Define approved alternatives, incoming checks and PCB revision identification. During factory and shipment review, verify model and labeling identity. The importer or responsible party should retain the required technical documentation and seek current market-specific advice.
Conclusion: turn the decision into a working plan
Freeze a representative configuration, identify applicable market requirements with qualified specialists, screen likely emission and immunity risks, and preserve the exact evidence sent for formal assessment. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements