Production Testing
End-of-Line Test Fixtures for RC Toys
An end-of-line station converts a product specification into a short repeatable check for the finished RC toy. The fixture is useful only when its limits are understood.
Direct answer: Design a product-specific sequence for power, pairing, drive, steering and included functions, then verify station calibration, operator training and failed-unit segregation. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Compliance Documents and Test Reports: Buyer Guide, RC Toy Pilot Orders: How to Test a Program Before Scaling, How to Prepare RC Toys for a Retailer Line Review.
1. Define the tested configuration
Test the same battery, controller and accessory arrangement that the consumer receives or an approved equivalent.
A bench supply can help engineering diagnose faults, but it does not prove that the packed battery and controller work together. State whether the station uses a reference transmitter, each packed controller or both at different points. Record which configuration is tested so a buyer understands what the end-of-line result actually covers.
During factory testing and shipment preparation, use define the tested configuration as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Write an observable sequence
List power-on, pairing, forward, reverse, left, right, stop and any lights, sounds or stunt modes.
The sequence should be short enough for production while still covering the defining functions. A wheel spin in the air may detect a dead motor but not poor traction or steering alignment under load. Add a sample-based floor test if the product risk justifies it. Define what counts as pass, borderline and fail instead of relying on operator intuition.
During factory testing and shipment preparation, use write an observable sequence as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Make the station hard to misuse
Use clear labels, controlled reference equipment and a physical layout that keeps tested and untested units apart.
A fixture can create false passes if the operator skips a step or presses the wrong button. Simple visual cues, a fixed order and an interlock where practical improve consistency. Keep cables and contacts in good condition; a worn test lead can make good toys look bad or hide a weak product connector.
During factory testing and shipment preparation, use make the station hard to misuse as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Check station repeatability
Run known-good and known-fault examples at the start of a shift and after maintenance.
This is a practical confidence check, not a claim of formal measurement-system certification. A fixture that silently drifts can release defects for hours. Record the verification result and the station identity. If a check fails, isolate products tested since the last known-good result and decide how to retest them.
During factory testing and shipment preparation, use check station repeatability as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Track failures by symptom
Separate no power, pairing, steering, drive, charging and accessory defects.
A single fail tally hides patterns that engineering could fix. Log the failure category and production lot without forcing operators to diagnose the root cause at the station. A spike in one symptom after a component change is an early warning. The line should have a clear route for repair, retest or scrap rather than returning uncertain units to the normal flow.
During factory testing and shipment preparation, use track failures by symptom as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Validate after packing steps
Consider whether packing can introduce errors not seen at the functional station.
A toy can pass the bench then be boxed with the wrong controller or without the charging cable. Final pack-out checks should verify model, color, accessories, manual and carton label against the purchase order. Do not use an electronics test result as a substitute for packaging or market-label review.
During factory testing and shipment preparation, use validate after packing steps as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Compare with independent inspection
Use pre-shipment samples to check the actual retail pack and selected functions outside the production station.
Factory end-of-line data supports process control, while buyer inspection checks whether the delivered batch matches the agreement. If the independent result conflicts with line records, investigate the fixture, sampling conditions and version identity. The objective is a traceable correction, not a debate over which checklist has a more impressive name.
During factory testing and shipment preparation, use compare with independent inspection as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
An importer visits a factory and hears that every RC stunt car receives a 100-percent test. At the station, the operator powers the car and spins the rear wheels for two seconds. That confirms some electrical functions but never checks steering, the flip mechanism or the packed controller. The buyer and factory rewrite the sequence around the functions customers actually purchase: power, pairing, forward, reverse, left, right and one complete stunt cycle. A known faulty unit is used to verify that the station can detect a defined failure. Rejected cars move to a marked holding area and are retested only after documented correction. Packing staff separately confirm the controller, cable and manual. The revised claim every car is function-tested now has a stated meaning, method and record. It still does not replace sample-based shipment inspection or market-specific testing.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISO 8124-1:2022 toy safety overview: Mechanical and physical safety considerations for toys.
Photography plan for this article
Article hero image — After the opening section
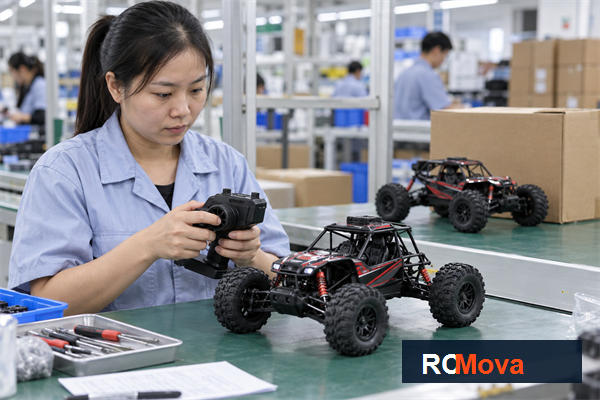
Image title: End-of-Line Test Fixtures for RC Toys — RC toy sourcing overview
Caption: Function checks and inspection records help keep an approved configuration consistent before packing. Article focus: rc toy end of line test.
ALT text: Asian quality inspector testing an RC vehicle at a Shenzhen factory inspection bench; rc toy end of line test buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for End-of-Line Test Fixtures for RC Toys, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
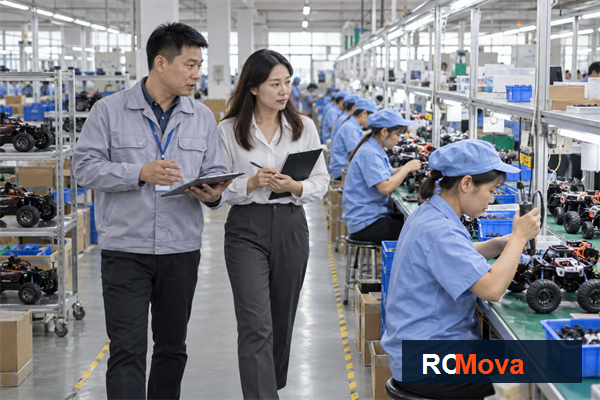
Image title: End-of-Line Test Fixtures for RC Toys — RC toy quality and shipment check
Caption: Production review for rc toy end of line test before the export handoff.
ALT text: Asian quality team reviewing rc toy end of line test with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy end of line test against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about define the tested configuration?
Test the same battery, controller and accessory arrangement that the consumer receives or an approved equivalent. A bench supply can help engineering diagnose faults, but it does not prove that the packed battery and controller work together. State whether the station uses a reference transmitter, each packed controller or both at different points. Record which configuration is tested so a buyer understands what the end-of-line result actually covers.
How should buyers verify check station repeatability?
Run known-good and known-fault examples at the start of a shift and after maintenance. This is a practical confidence check, not a claim of formal measurement-system certification. A fixture that silently drifts can release defects for hours. Record the verification result and the station identity. If a check fails, isolate products tested since the last known-good result and decide how to retest them.
What should be confirmed before shipment?
Use pre-shipment samples to check the actual retail pack and selected functions outside the production station. Factory end-of-line data supports process control, while buyer inspection checks whether the delivered batch matches the agreement. If the independent result conflicts with line records, investigate the fixture, sampling conditions and version identity. The objective is a traceable correction, not a debate over which checklist has a more impressive name.
Conclusion: turn the decision into a working plan
Design a product-specific sequence for power, pairing, drive, steering and included functions, then verify station calibration, operator training and failed-unit segregation. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements