Plastic Part Quality
Injection-Molded RC Toy Parts: Defect Review
Molded RC toy parts should be judged in their final assembled role. A surface mark, a dimensional error and a sharp flash edge have different consequences.
Direct answer: Create part-specific visual and fit criteria, inspect representative cavities and verify that corrections preserve the approved vehicle function. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Spare Parts Strategy for Distributors and Private Labels, What Should Buyers Check for Parts and Accessories When Sourcing Remote Control Toys?, What Should Buyers Check for Parts and Accessories When Sourcing RC Toys?.
1. Classify defects by consequence
Separate safety concerns, assembly failures, visible cosmetic variation and minor non-visible marks.
A thin flash edge near a child’s grip is different from a small internal flow line. Define where the part is visible and touched, and whether it carries a wheel, battery door or screw. A consistent classification lets the factory prioritize correction and helps buyers avoid rejecting an entire lot for harmless variation while missing a structural problem.
During factory testing and shipment preparation, use classify defects by consequence as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Inspect fit before appearance
Assemble the shell, chassis, axle supports and battery cover using normal production tools.
Warp can be subtle on a loose part but obvious when screws pull the shell into place or a wheel rubs after assembly. Use a gauge or mating part at critical interfaces. Check both sides of a multi-cavity run because one cavity can drift while another remains stable. A clean painted exterior cannot compensate for an unreliable wheel mount.
During factory testing and shipment preparation, use inspect fit before appearance as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Document the visual standard
Photograph acceptable and unacceptable examples under controlled light and viewing distance.
Terms such as slight sink or normal flash are too subjective on their own. Mark inspection zones and define what is permitted in each. Keep the examples tied to the exact resin color and texture, since gloss can make a small mark more visible. A practical standard also reduces argument at pre-shipment inspection.
During factory testing and shipment preparation, use document the visual standard as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Trace recurring patterns
Record cavity, machine, date and material lot when the same defect repeats.
A short shot on one detail may follow an inconsistent gate, while variable sink can be affected by wall thickness and cooling. The buyer does not need to dictate molding settings, but should expect the factory to connect observations with process evidence. Repeated rework without a stable cause creates hidden schedule and quality risk.
During factory testing and shipment preparation, use trace recurring patterns as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Assess post-molding operations
Check painting, pad printing, trimming and assembly after the raw plastic review.
A part can meet dimensions before paint but fail fit after a heavy coating or an aggressive trim. Inspect decoration registration and edge condition on finished units. If a change in paint or adhesive affects appearance or odor, keep the approved material record current and let a qualified adviser assess market-specific requirements.
During factory testing and shipment preparation, use assess post-molding operations as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Approve correction on the complete toy
Compare the corrected part with the golden sample and rerun affected vehicle checks.
Trimming flash may improve appearance but weaken a clip; changing a mold insert may alter wheel alignment. Ask for before-and-after samples and a written description of the fix. This is especially important when correction happens during a tight delivery window and several teams assume someone else validated the result.
During factory testing and shipment preparation, use approve correction on the complete toy as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Use inspection data to decide release
Sample finished products across the batch and hold any uncertain cavity or lot until disposition is clear.
A single perfect first-off part does not prove the rest of the run. Review defect frequency and location with the agreed acceptance plan, and distinguish reworkable cosmetic issues from performance or safety concerns. Keep the release decision, sample size and corrective evidence with the shipment record.
During factory testing and shipment preparation, use use inspection data to decide release as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A buyer inspecting painted RC trucks notices a slight surface sink near the hood on some units. The same lot also contains chassis pieces that twist enough to make one front wheel rub. Treating both as one cosmetic defect would miss the functional risk. The factory sorts by molded part and cavity, checks the chassis in a complete assembled vehicle and compares hood appearance with the approved visual standard. The buyer may accept a defined minor hood mark while requiring correction and retest of wheel alignment. Any molding-process adjustment is validated on finished parts across a representative run. This separation keeps acceptance proportional: the team does not reject every harmless visual variation, but it does not allow a smooth paint job to hide poor fit. The release record states which lots were checked and how nonconforming units were handled.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISO 8124-1:2022 toy safety overview: Mechanical and physical safety considerations for toys.
Photography plan for this article
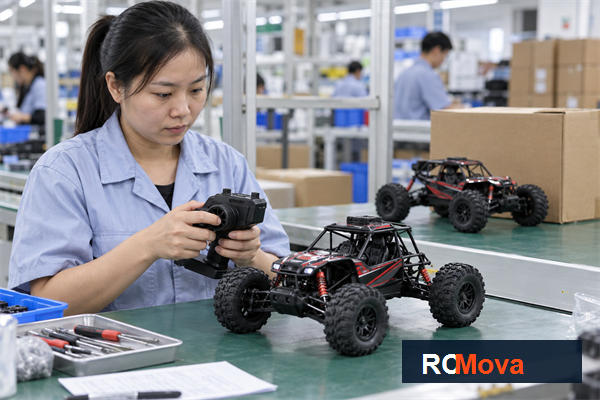
Article hero image — After the opening section
Image title: Injection-Molded RC Toy Parts: Defect Review — RC toy sourcing overview
Caption: Function checks and inspection records help keep an approved configuration consistent before packing. Article focus: rc toy injection molding defects.
ALT text: Asian quality inspector testing an RC vehicle at a Shenzhen factory inspection bench; rc toy injection molding defects buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for Injection-Molded RC Toy Parts: Defect Review, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
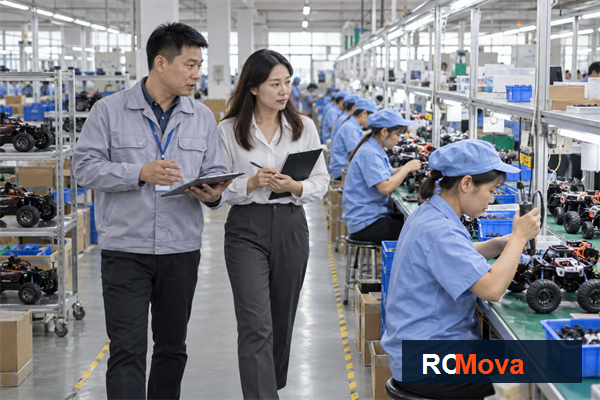
In-article supporting image — Before the FAQ section
Image title: Injection-Molded RC Toy Parts: Defect Review — RC toy quality and shipment check
Caption: Production review for rc toy injection molding defects before the export handoff.
ALT text: Asian quality team reviewing rc toy injection molding defects with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy injection molding defects against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about classify defects by consequence?
Separate safety concerns, assembly failures, visible cosmetic variation and minor non-visible marks. A thin flash edge near a child’s grip is different from a small internal flow line. Define where the part is visible and touched, and whether it carries a wheel, battery door or screw. A consistent classification lets the factory prioritize correction and helps buyers avoid rejecting an entire lot for harmless variation while missing a structural problem.
How should buyers verify trace recurring patterns?
Record cavity, machine, date and material lot when the same defect repeats. A short shot on one detail may follow an inconsistent gate, while variable sink can be affected by wall thickness and cooling. The buyer does not need to dictate molding settings, but should expect the factory to connect observations with process evidence. Repeated rework without a stable cause creates hidden schedule and quality risk.
What should be confirmed before shipment?
Sample finished products across the batch and hold any uncertain cavity or lot until disposition is clear. A single perfect first-off part does not prove the rest of the run. Review defect frequency and location with the agreed acceptance plan, and distinguish reworkable cosmetic issues from performance or safety concerns. Keep the release decision, sample size and corrective evidence with the shipment record.
Conclusion: turn the decision into a working plan
Create part-specific visual and fit criteria, inspect representative cavities and verify that corrections preserve the approved vehicle function. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements