Production Control
RC Toy Line Clearance and SKU Changeover Control
Line clearance is the documented removal and reconciliation of the previous product before the next SKU begins. For RC toys, the process should cover components, radio sets, artwork, labels, work instructions and packed goods.
Direct answer: Define changeover boundaries, reconcile old material and approve the first new SKU unit before normal production resumes. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Factories and buyers need to prevent controllers, colors, labels, manuals and packaging from one SKU entering another during production changeover. Mixed versions can pass basic function testing but create compliance, barcode, language and customer-order errors.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Engineering Change Control During Production, RC Toy Quality Control Checklist for B2B Orders, How to Choose a Remote Control System for an RC Toy.
1. Define the SKU boundary
List every difference between the outgoing and incoming model, including hidden electronics and market documents.
Color alone is not enough. Compare controller pairing, battery, accessories, labels, manual language, barcode and carton marks. Use the product master and approved samples as the changeover reference.
During factory testing and shipment preparation, use define the sku boundary as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Stop and segregate output
Set a clear last-good unit and prevent unfinished old SKU material from blending with the next run.
Mark work in process and quarantine uncertain items. Do not rely on operators remembering which tray belongs to which order. Physical zones and identifiers should remain visible through packing.
During factory testing and shipment preparation, use stop and segregate output as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Remove and reconcile materials
Return, count or dispose of old components, labels, manuals and packaging under controlled rules.
Printed items deserve particular attention because one piece can create a market or barcode error. Record discrepancies and investigate unexplained balances. Protect reusable components from losing lot identity.
During factory testing and shipment preparation, use remove and reconcile materials as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Change documents and settings
Replace work instructions, visual aids, test programs, printers and equipment settings with the approved new revision.
Electronic screens can retain an old file even when paper is changed. Use access control and version checks. Confirm radio or functional settings before the first article.
During factory testing and shipment preparation, use change documents and settings as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Inspect the first new SKU
Review identity, function and a complete closed pack before routine output is authorized.
The first-piece check should include the vehicle, controller, battery arrangement, accessories, labels, manual, barcode and master carton. Check several consecutive units after a complex transition.
During factory testing and shipment preparation, use inspect the first new sku as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Maintain separation during production
Control material replenishment, temporary storage, repair and rework so old SKU items do not return to the line.
Rework areas are common mixing points. Identify the product and disposition before it leaves the main flow. Mixed-order days may require dedicated racks or timed production blocks.
During factory testing and shipment preparation, use maintain separation during production as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Verify packed-goods reconciliation
Compare final SKU quantities, unused printed material and carton labels with the order before shipment release.
A packing audit can detect patterns missed by random function checks. Resolve unknown cartons and scan product identifiers where the system supports it. Retain the changeover record with production and inspection evidence.
During factory testing and shipment preparation, use verify packed-goods reconciliation as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A factory changes from a blue RC car for one market to a red version for another. Vehicle bodies are separated, but a carton of old-language manuals remains under the packing bench and enters the new run. In this illustrative scenario, the next changeover uses area zones, material count-back and a signed first-pack review. The line is not released until the vehicle, controller, manual, barcode and case label all match the new SKU.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISO quality management guidance on external providers: Official ISO auditing guidance on controlling externally provided products and services.
Photography plan for this article
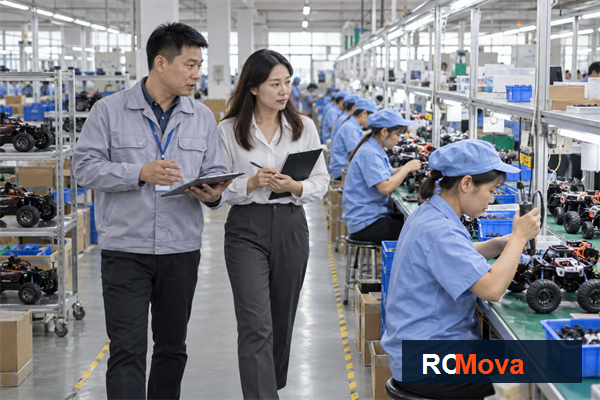
Article hero image — After the opening section
Image title: RC Toy Line Clearance and SKU Changeover Control — RC toy sourcing overview
Caption: A factory audit is more useful when buyers follow the product flow from assembly through packing. Article focus: rc toy line clearance.
ALT text: Asian buyer and factory supervisor reviewing an RC toy production line in Shenzhen; rc toy line clearance buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Line Clearance and SKU Changeover Control, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
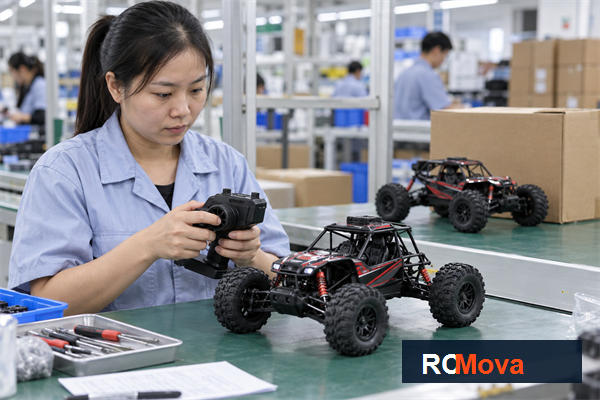
In-article supporting image — Before the FAQ section
Image title: RC Toy Line Clearance and SKU Changeover Control — RC toy quality and shipment check
Caption: Production review for rc toy line clearance before the export handoff.
ALT text: Asian quality team reviewing rc toy line clearance with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy line clearance against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about define the sku boundary?
List every difference between the outgoing and incoming model, including hidden electronics and market documents. Color alone is not enough. Compare controller pairing, battery, accessories, labels, manual language, barcode and carton marks. Use the product master and approved samples as the changeover reference.
How should buyers verify change documents and settings?
Replace work instructions, visual aids, test programs, printers and equipment settings with the approved new revision. Electronic screens can retain an old file even when paper is changed. Use access control and version checks. Confirm radio or functional settings before the first article.
What should be confirmed before shipment?
Compare final SKU quantities, unused printed material and carton labels with the order before shipment release. A packing audit can detect patterns missed by random function checks. Resolve unknown cartons and scan product identifiers where the system supports it. Retain the changeover record with production and inspection evidence.
Conclusion: turn the decision into a working plan
Define changeover boundaries, reconcile old material and approve the first new SKU unit before normal production resumes. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements