Ocean Freight Protection
RC Toy Ocean Freight Moisture and Carton Control
Moisture control for RC toy shipments requires dry goods, suitable packaging, a clean container and a route-specific plan. Desiccants cannot compensate for wet cartons, active leaks or unapproved materials packed at high moisture.
Direct answer: Assess moisture sources across packing, loading, voyage and receiving, then document carton condition, container inspection and proportionate controls for the actual route. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Buyers need to reduce moisture-related carton, printing, metal-part and product damage during long ocean movements and storage handoffs. Dry factory cartons can encounter temperature changes, condensation, wet floors or high-humidity storage before the buyer receives them.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Quality Control Checklist for B2B Orders, How to Choose a Remote Control System for an RC Toy, How Should Buyers Choose Remote Control Toys?.
1. Map the moisture pathway
Review raw cartons, packed-goods storage, container condition, voyage climate and destination warehousing as one chain.
A problem blamed on the ocean may begin with damp corrugated board or outdoor staging before loading. Record where cartons wait and how long. Use route and season information to decide which controls deserve attention.
During factory testing and shipment preparation, use map the moisture pathway as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Confirm dry product and packaging
Check that cartons, inserts, manuals and product surfaces are dry and conditioned before sealing.
Trapping moisture inside a polybag or closed carton can shift the problem inward. Set practical storage and packing conditions with packaging specialists. Do not apply a universal humidity number without relating it to materials, method and market requirements.
During factory testing and shipment preparation, use confirm dry product and packaging as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Inspect the empty container
Review roof, walls, doors, seals, floor, odor and evidence of previous water entry before loading.
Photograph the container number and representative surfaces. Reject or escalate visible holes, standing water, damaged seals or contaminated interiors. A clean appearance alone does not guarantee suitability, but it creates an important release checkpoint.
During factory testing and shipment preparation, use inspect the empty container as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Select justified moisture controls
Choose liners, barriers, desiccants or ventilation approaches with qualified logistics and packaging advice.
Quantity and placement depend on route, duration, temperature change, packaging permeability and cargo moisture. Keep control materials away from products when leakage, dust or contact could cause damage. Record exactly what was installed.
During factory testing and shipment preparation, use select justified moisture controls as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Maintain carton strength
Evaluate whether humidity exposure and stacking can reduce compression performance during transport.
A carton may pass a dry warehouse stack check yet weaken under sustained moisture. Use realistic distribution testing where the risk justifies it. Avoid reducing board grade or internal support solely to gain cube without reconsidering voyage exposure.
During factory testing and shipment preparation, use maintain carton strength as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Document loading condition
Photograph dry floors, carton condition, wall clearance where used, control placement and final door closure.
The record should identify date, container and order. It is not proof that damage cannot occur, but it helps distinguish preparation from later events. Keep carton lots and packing times traceable when multiple days of goods are combined.
During factory testing and shipment preparation, use document loading condition as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Prepare receiving and claims evidence
Give the warehouse a procedure for seal check, container photographs, damage isolation and prompt notice.
Do not discard wet cartons or control materials before the insurer or carrier evidence requirements are understood. Count affected SKUs separately and inspect the product, electronics and metal parts rather than assuming cosmetic carton damage is the only issue.
During factory testing and shipment preparation, use prepare receiving and claims evidence as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
An importer receives RC trucks with softened master cartons and spotting on printed display boxes near one container wall. The factory records show dry cartons at packing, but no empty-container inspection or loading-floor photograph was retained. In this illustrative scenario, the next shipment adds storage humidity checks, carton conditioning, a documented container review and agreed placement of appropriate moisture controls. Receiving staff photograph the seal and doors before unloading, creating evidence for prevention and any future claim.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISTA transport packaging test procedures: Official overview of package integrity and distribution simulation procedures.
Photography plan for this article
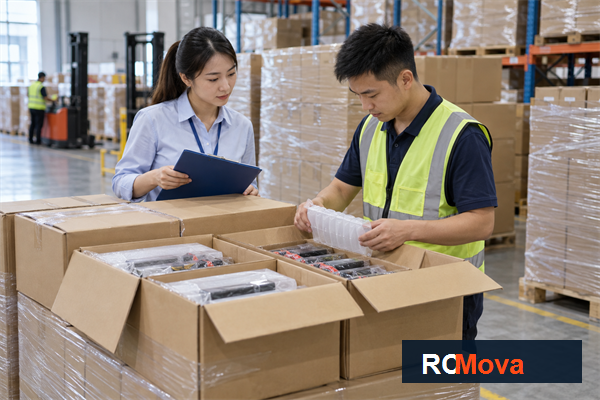
Article hero image — After the opening section
Image title: RC Toy Ocean Freight Moisture and Carton Control — RC toy sourcing overview
Caption: Battery-related shipment planning should be checked against the actual product and packing configuration. Article focus: rc toy ocean freight moisture.
ALT text: Asian logistics staff checking packed RC toy export cartons in a Shenzhen warehouse; rc toy ocean freight moisture buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Ocean Freight Moisture and Carton Control, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
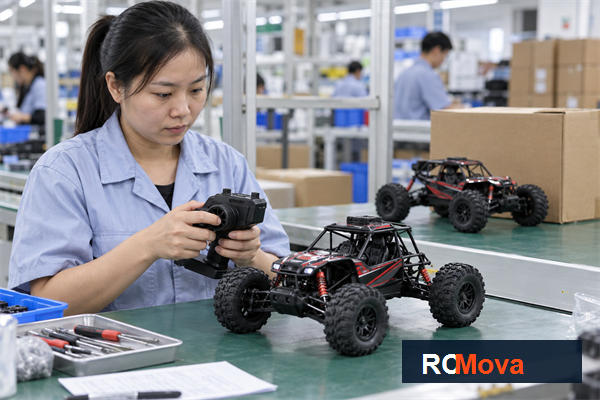
In-article supporting image — Before the FAQ section
Image title: RC Toy Ocean Freight Moisture and Carton Control — RC toy quality and shipment check
Caption: Production review for rc toy ocean freight moisture before the export handoff.
ALT text: Asian quality team reviewing rc toy ocean freight moisture with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy ocean freight moisture against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about map the moisture pathway?
Review raw cartons, packed-goods storage, container condition, voyage climate and destination warehousing as one chain. A problem blamed on the ocean may begin with damp corrugated board or outdoor staging before loading. Record where cartons wait and how long. Use route and season information to decide which controls deserve attention.
How should buyers verify select justified moisture controls?
Choose liners, barriers, desiccants or ventilation approaches with qualified logistics and packaging advice. Quantity and placement depend on route, duration, temperature change, packaging permeability and cargo moisture. Keep control materials away from products when leakage, dust or contact could cause damage. Record exactly what was installed.
What should be confirmed before shipment?
Give the warehouse a procedure for seal check, container photographs, damage isolation and prompt notice. Do not discard wet cartons or control materials before the insurer or carrier evidence requirements are understood. Count affected SKUs separately and inspect the product, electronics and metal parts rather than assuming cosmetic carton damage is the only issue.
Conclusion: turn the decision into a working plan
Assess moisture sources across packing, loading, voyage and receiving, then document carton condition, container inspection and proportionate controls for the actual route. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements