Retail Packaging
Shelf-Ready Display Packaging for RC Toys
Shelf-ready packaging should help a store move an RC toy from a shipping carton to a shopper-facing display without losing product identification or protection.
Direct answer: Prototype the display from the finished product and shelf dimensions, then validate opening, replenishment, barcode access and transport performance before bulk printing. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see Custom RC Toy Packaging Guide for Private-Label Buyers, Custom RC Toy Packaging for Export: Buyer Requirements Guide, RC Toy Packaging Warnings and Manual Requirements: Buyer Guide.
1. Start with the retailer fixture
Request shelf width, depth, height, facing count and any store-specific display rules.
The same remote control car can look attractive in a rendering yet fail to fit the actual shelf. Work from the closed retail pack and a measured fixture. Confirm whether the store expects an open tray, removable shipper top or freestanding unit. Keep a small tolerance for real carton variation and do not design to a perfect mathematical fit that blocks replenishment.
During factory testing and shipment preparation, use start with the retailer fixture as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Make setup intuitive
Design the carton so a store employee can open and position it without tools or lengthy instructions.
A tear strip that damages the visible tray, exposes sharp edges or scatters loose accessories defeats the labor-saving purpose. Test setup with a person who did not design the pack. Observe the sequence and record where they hesitate. This practical trial often finds more useful issues than approving only a digital dieline or an attractive printed mockup.
During factory testing and shipment preparation, use make setup intuitive as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Protect the toy while displaying it
Keep wheels, controllers, antennas and decorative parts secure through handling and transit.
Open-front displays can leave vulnerable areas exposed. Review how the vehicle is retained before and after the shipping cover is removed, and whether a customer can lift one unit without destabilizing the others. Use the intended vehicle weight and center of gravity when assessing tray strength. If a design needs additional ties or inserts, include their removal in the store setup trial.
During factory testing and shipment preparation, use protect the toy while displaying it as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Keep identity visible at each level
Place consumer, tray and outer-carton identifiers where receiving and shelf teams can use them.
A display shipper may be an orderable unit while its contained toys are the consumer units. The retailer must be able to count contents and scan the appropriate level without opening every box. Review barcode contrast, quiet zones and placement on the actual printed stock. Do not let a promotional graphic hide a required product name, age warning or stock-keeping reference.
During factory testing and shipment preparation, use keep identity visible at each level as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Validate transport and shelf use separately
Test the closed shipper for distribution hazards and the opened display for store stability.
A transport test is not a shelf-use test. The ISTA procedure must match the expected shipping route, and its result should be reported for the exact packed configuration. Then examine the opened tray for sagging, tipping and product access. A pass on an earlier plain carton does not automatically cover a new perforated display design.
During factory testing and shipment preparation, use validate transport and shelf use separately as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Cost the whole store operation
Compare material and freight cost with setup labor, damage exposure and replenishment speed.
A tray can save store labor while adding bulk to the master carton. Model units per case and pallet, including any increase in dimensional freight. Ask the retail partner which benefit matters most: faster stocking, stronger brand block, less damage or simpler inventory. This avoids paying for structural features that the channel cannot use.
During factory testing and shipment preparation, use cost the whole store operation as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Approve the production sample
Inspect a filled, printed and shipped representative pack before authorizing the bulk run.
Check cut lines, tear behavior, glue joints, color, count and product retention on real material. Record photographs of the closed and opened states. At final shipment inspection, sample finished cases and verify that the store setup still matches the approved reference. A change in board grade or inner insert should trigger a new review rather than being treated as a cosmetic substitution.
During factory testing and shipment preparation, use approve the production sample as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
Imagine a buyer requesting a six-unit open tray for a holiday RC car promotion. The first artwork mockup looks strong, but a filled prototype reveals that the cars lean forward when the shipper lid is removed. Store staff also tear the tray wall while following an unmarked perforation. The next review should involve a real shelf, filled boxes and a person who has not seen the design before. The team may deepen the tray, move the tear line or lower the product center of gravity. Those changes will alter carton size and perhaps pallet count, so the freight calculation and retailer item data need updating. A transit simulation on the final closed pack, followed by a stability check on the opened tray, gives two different kinds of evidence. Approval should attach to that physical configuration, not the original rendering. This is why shelf-ready packaging is a channel operations project, not only a graphic design project.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISTA transport packaging test procedures: Official overview of package integrity and distribution simulation procedures.
Photography plan for this article
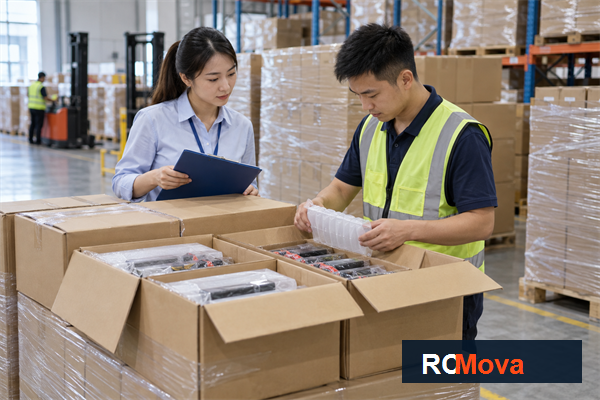
Article hero image — After the opening section
Image title: Shelf-Ready Display Packaging for RC Toys — RC toy sourcing overview
Caption: Battery-related shipment planning should be checked against the actual product and packing configuration. Article focus: rc toy shelf ready packaging.
ALT text: Asian logistics staff checking packed RC toy export cartons in a Shenzhen warehouse; rc toy shelf ready packaging buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for Shelf-Ready Display Packaging for RC Toys, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
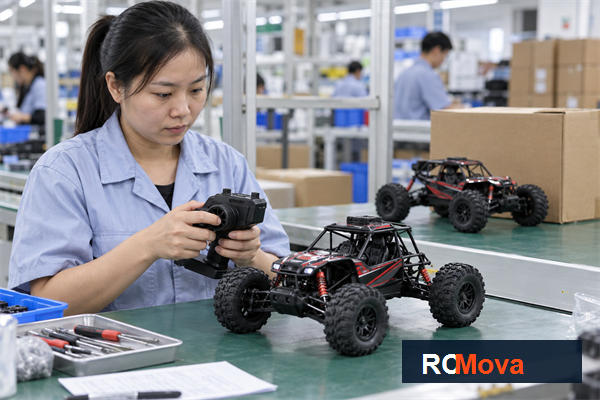
Image title: Shelf-Ready Display Packaging for RC Toys — RC toy quality and shipment check
Caption: Production review for rc toy shelf ready packaging before the export handoff.
ALT text: Asian quality team reviewing rc toy shelf ready packaging with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy shelf ready packaging against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about start with the retailer fixture?
Request shelf width, depth, height, facing count and any store-specific display rules. The same remote control car can look attractive in a rendering yet fail to fit the actual shelf. Work from the closed retail pack and a measured fixture. Confirm whether the store expects an open tray, removable shipper top or freestanding unit. Keep a small tolerance for real carton variation and do not design to a perfect mathematical fit that blocks replenishment.
How should buyers verify keep identity visible at each level?
Place consumer, tray and outer-carton identifiers where receiving and shelf teams can use them. A display shipper may be an orderable unit while its contained toys are the consumer units. The retailer must be able to count contents and scan the appropriate level without opening every box. Review barcode contrast, quiet zones and placement on the actual printed stock. Do not let a promotional graphic hide a required product name, age warning or stock-keeping reference.
What should be confirmed before shipment?
Inspect a filled, printed and shipped representative pack before authorizing the bulk run. Check cut lines, tear behavior, glue joints, color, count and product retention on real material. Record photographs of the closed and opened states. At final shipment inspection, sample finished cases and verify that the store setup still matches the approved reference. A change in board grade or inner insert should trigger a new review rather than being treated as a cosmetic substitution.
Conclusion: turn the decision into a working plan
Prototype the display from the finished product and shelf dimensions, then validate opening, replenishment, barcode access and transport performance before bulk printing. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements