Assembly Reliability
RC Toy Wire Routing and Strain-Relief Inspection
Wire routing is a design and assembly control. The approved path should protect conductors and connectors from sharp edges, moving parts, heat, fasteners and repeated user handling.
Direct answer: Define routing and strain-relief references in the product design, verify them at first article and use targeted in-process checks before the body closes the assembly. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Quality teams need to prevent pinched, rubbing, loose or overstressed wires from causing intermittent power, charging or steering failures. A finished toy can pass a short function test while internal routing is vulnerable to vibration, body movement or repeated battery access.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see Pre-Shipment Inspection for RC Toys: A Buyer’s Practical Guide, RC Toy Quality Inspection and Defect Checks: Buyer Guide, RC Toy Cosmetic and Assembly Quality: Inspection Guide.
1. Map every harness path
Identify battery, motor, charging, switch, lighting and steering wires through the assembled product.
Use drawings and photographs that show connector orientation and routing features. Note moving suspension, gears, shafts, body screws and battery doors. Product revisions need their own controlled reference.
During factory testing and shipment preparation, use map every harness path as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Design suitable strain relief
Support wires near connectors, solder joints and user-handled exits without creating a sharp bend or damaging insulation.
The method may include geometry, clips, ties, sleeves or approved adhesive. Engineering should consider service and assembly variability. Do not add an uncontrolled blob of adhesive as a line-side fix.
During factory testing and shipment preparation, use design suitable strain relief as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Prevent pinch and abrasion
Maintain clearance from edges, screw bosses, closing shells and moving drivetrain parts.
A wire may move during assembly, so fixtures or visual aids should hold the intended path. Inspect after the housing is fastened where possible. Protect edges and verify that wires are not carrying structural load.
During factory testing and shipment preparation, use prevent pinch and abrasion as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Control connector assembly
Check terminal seating, polarity, latch engagement, crimp or solder workmanship and mating force.
Similar connectors can be reversed or incompletely inserted. Use keyed parts and clear instructions where practical. A pull check needs a defined safe method that does not damage accepted assemblies.
During factory testing and shipment preparation, use control connector assembly as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Verify repeated access
Cycle battery doors, removable packs, charging leads or body removal under expected user handling.
Observe twist, bend radius and contact with covers. Include the controller when its battery leads or contacts require review. Stop if insulation damage or unusual heat appears.
During factory testing and shipment preparation, use verify repeated access as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Inspect before closure
Place the main routing check at the stage where wires remain visible and corrections are controlled.
Final external inspection cannot see an internal pinch. Record first-piece approval and sample frequency based on risk. Reopened units should repeat the relevant function and closure checks.
During factory testing and shipment preparation, use inspect before closure as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Link failures to root cause
Use lot, location, wire condition and assembly evidence when investigating intermittent or no-power complaints.
Replacing a battery may temporarily hide a routing issue. Preserve failed parts and photographs. Feed confirmed findings into design, supplier and work-instruction changes, then verify the next production run.
During factory testing and shipment preparation, use link failures to root cause as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
An RC truck passes final driving tests, but some field units lose power after repeated battery changes. Investigation finds a wire bending tightly where it leaves the pack connector, with no consistent strain relief. In this illustrative scenario, engineering changes the routing feature, the work instruction adds a photograph and first production units receive a controlled pull-and-bend review. The corrected design is rechecked in the full product rather than treated as a cosmetic assembly fix.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see IPC document revision table: Official listing of electronics assembly and inspection standards, including IPC-A-610.
Photography plan for this article
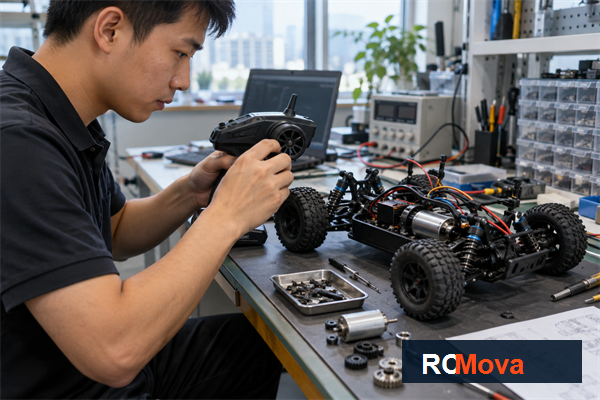
Article hero image — After the opening section
Image title: RC Toy Wire Routing and Strain-Relief Inspection — RC toy sourcing overview
Caption: Controller selection should be tested as part of the complete vehicle and user experience. Article focus: rc toy wire routing.
ALT text: Asian electronics technician testing an RC controller and vehicle components; rc toy wire routing buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Wire Routing and Strain-Relief Inspection, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
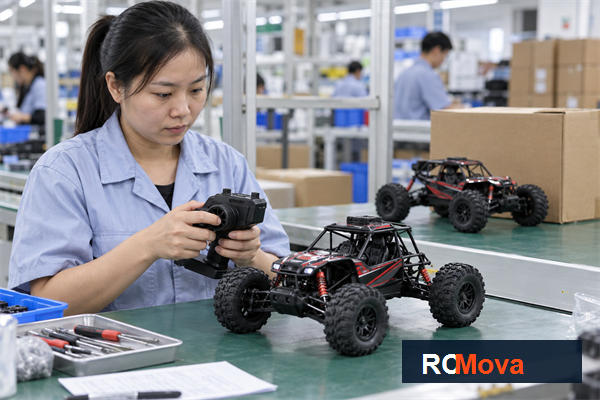
In-article supporting image — Before the FAQ section
Image title: RC Toy Wire Routing and Strain-Relief Inspection — RC toy quality and shipment check
Caption: Production review for rc toy wire routing before the export handoff.
ALT text: Asian quality team reviewing rc toy wire routing with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy wire routing against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about map every harness path?
Identify battery, motor, charging, switch, lighting and steering wires through the assembled product. Use drawings and photographs that show connector orientation and routing features. Note moving suspension, gears, shafts, body screws and battery doors. Product revisions need their own controlled reference.
How should buyers verify control connector assembly?
Check terminal seating, polarity, latch engagement, crimp or solder workmanship and mating force. Similar connectors can be reversed or incompletely inserted. Use keyed parts and clear instructions where practical. A pull check needs a defined safe method that does not damage accepted assemblies.
What should be confirmed before shipment?
Use lot, location, wire condition and assembly evidence when investigating intermittent or no-power complaints. Replacing a battery may temporarily hide a routing issue. Preserve failed parts and photographs. Feed confirmed findings into design, supplier and work-instruction changes, then verify the next production run.
Conclusion: turn the decision into a working plan
Define routing and strain-relief references in the product design, verify them at first article and use targeted in-process checks before the body closes the assembly. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements