Supply Continuity
RC Toy Component Shortages: Order Contingency Plan
A component shortage is a project-control problem. The right response protects the approved product and the delivery promise rather than silently replacing a part.
Direct answer: Identify long-lead components before order release, set escalation thresholds and require written approval for any substitute that affects the finished RC toy. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Supplier Business Continuity Planning, RC Toy Sourcing Checklist: What to Confirm Before You Place an Order, RC Toy MOQ Guide: How Buyers Should Discuss Minimum Order Quantities.
1. Map the constrained parts
Ask which motors, PCBs, radio modules, cells, connectors and printed materials drive the critical path.
Not every part deserves the same attention. A standard screw may be easy to replenish while a controller chip or decorated shell can stop a full line. Request a bill-of-material risk view with lead time, approved source and available stock for the specific order. Do not infer supply security from a generic factory capacity figure.
During factory testing and shipment preparation, use map the constrained parts as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Connect shortages to milestones
Set dates for component commitment, sample lock, production start, inspection and shipping handoff.
A shortage discovered after retail artwork is printed leaves fewer safe alternatives than one found during quotation. Ask the supplier to report material readiness before assembly begins and to flag missed milestones immediately. The buyer should know which delay consumes float and which delay moves the launch date. A revised schedule must show the new critical path, not only a new final date.
During factory testing and shipment preparation, use connect shortages to milestones as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Define substitution rules
Treat any proposed alternate part as a controlled engineering change with a documented impact review.
A battery pack that fits the cavity may still change runtime, charging behavior, labeling or transport documents. A motor from another supplier may change heat and noise. Compare specifications, approved sample behavior, safety evidence, cost and service compatibility. Do not approve a change only because the part number is described as equivalent by a sales contact.
During factory testing and shipment preparation, use define substitution rules as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Prioritize customer commitments
Rank SKUs and channels by actual launch consequence before reallocating scarce components.
A promotional item with a fixed event date can have a different tolerance from replenishment stock. Document which purchase orders receive available material and why, then tell affected buyers promptly. Partial production may help, but mixed versions within one retail SKU can confuse documentation and after-sales support. The buyer should approve any split delivery or version boundary.
During factory testing and shipment preparation, use prioritize customer commitments as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Keep evidence of the revised product
If a substitute is approved, update samples, test plans, component records and pack-out references.
The finished units should be distinguishable from earlier versions where the difference matters. Factory testing needs to check the changed function on production samples, and market-specific compliance should be reviewed by qualified advisers. An updated bill of materials alone does not prove that a full toy set still behaves or ships in the same way.
During factory testing and shipment preparation, use keep evidence of the revised product as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Compare recovery options honestly
Evaluate expedite fees, alternate suppliers, delayed launch and reduced assortment on the same decision sheet.
An airfreight rescue can erase margin or create battery-shipping complications. A color change may be cheaper but damage retailer item setup. Estimate the cost and operational consequences of each option, state what is known and what remains uncertain, and agree a decision deadline. The factory should not assume the buyer prefers the fastest option at any price.
During factory testing and shipment preparation, use compare recovery options honestly as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Build a reorder lesson
After the shipment, update lead-time assumptions and approved alternates for the next order.
A one-time shortage does not necessarily justify permanent dual sourcing, but repeated risk should appear in future planning. Keep records of actual delay, customer impact and how the chosen response performed. This turns a difficult order into a more reliable replenishment program instead of repeating the same escalation every season.
During factory testing and shipment preparation, use build a reorder lesson as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A private-label RC truck is due for a seasonal promotion. Three weeks before assembly, the approved motor supplier reports a delay. The factory proposes a different motor with the same nominal voltage. The purchasing team could accept immediately to protect the date, but the alternative may change speed, heat or battery runtime. A controlled response compares the two motors in the approved truck with the intended battery and gearbox, checks documentation implications and calculates the revised production and freight dates. The buyer may choose a delayed complete order, a smaller first delivery using available approved motors, or a formally qualified alternate. Every option has a commercial cost. The selected plan should state which lots use which motor and what the retailer has been told. A verbal promise that the replacement is equivalent is not a sufficient release record.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISO quality management guidance on external providers: Official ISO auditing guidance on controlling externally provided products and services.
Photography plan for this article
Article hero image — After the opening section
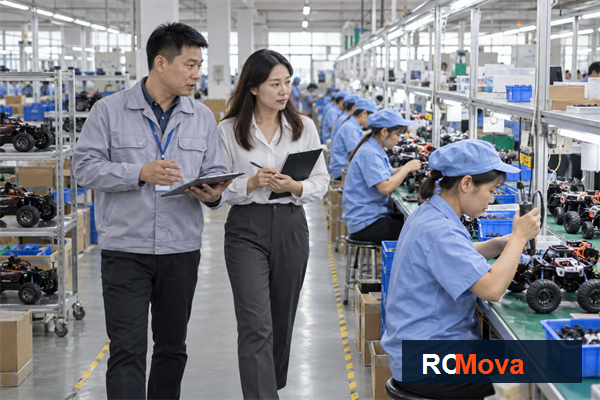
Image title: RC Toy Component Shortages: Order Contingency Plan — RC toy sourcing overview
Caption: A factory audit is more useful when buyers follow the product flow from assembly through packing. Article focus: rc toy component shortage plan.
ALT text: Asian buyer and factory supervisor reviewing an RC toy production line in Shenzhen; rc toy component shortage plan buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Component Shortages: Order Contingency Plan, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
In-article supporting image — Before the FAQ section
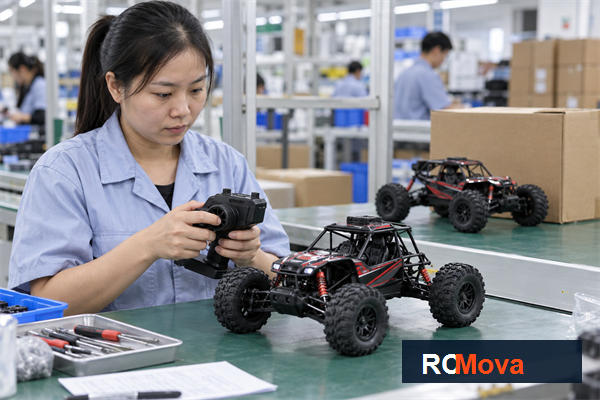
Image title: RC Toy Component Shortages: Order Contingency Plan — RC toy quality and shipment check
Caption: Production review for rc toy component shortage plan before the export handoff.
ALT text: Asian quality team reviewing rc toy component shortage plan with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy component shortage plan against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about map the constrained parts?
Ask which motors, PCBs, radio modules, cells, connectors and printed materials drive the critical path. Not every part deserves the same attention. A standard screw may be easy to replenish while a controller chip or decorated shell can stop a full line. Request a bill-of-material risk view with lead time, approved source and available stock for the specific order. Do not infer supply security from a generic factory capacity figure.
How should buyers verify prioritize customer commitments?
Rank SKUs and channels by actual launch consequence before reallocating scarce components. A promotional item with a fixed event date can have a different tolerance from replenishment stock. Document which purchase orders receive available material and why, then tell affected buyers promptly. Partial production may help, but mixed versions within one retail SKU can confuse documentation and after-sales support. The buyer should approve any split delivery or version boundary.
What should be confirmed before shipment?
After the shipment, update lead-time assumptions and approved alternates for the next order. A one-time shortage does not necessarily justify permanent dual sourcing, but repeated risk should appear in future planning. Keep records of actual delay, customer impact and how the chosen response performed. This turns a difficult order into a more reliable replenishment program instead of repeating the same escalation every season.
Conclusion: turn the decision into a working plan
Identify long-lead components before order release, set escalation thresholds and require written approval for any substitute that affects the finished RC toy. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements