Supply Continuity
RC Toy Supplier Business Continuity Planning
A business continuity plan explains how a supplier recognizes disruption, protects people and assets, communicates priorities and restores an acceptable production route. It should be tied to the buyer’s critical products and dates.
Direct answer: Identify single points of failure, define recovery priorities and evidence, and agree buyer communication and product requalification before an alternate process is used. This guide is written for importers, distributors, retailers and private-label teams that need to make a defensible buying decision before they approve an RC toy sample or release an order.
How procurement teams should use this guide
Buyer situation: Importers need to know how critical RC toy orders will be protected or recovered after equipment, utility, labor, logistics or supplier disruptions. A component-shortage plan does not cover the wider operational events that can stop tooling, records, testing, packing or shipment release.
Use the sections below as a discussion framework for the exact product and destination, not as a universal specification. Begin with the approved vehicle, controller, battery, accessories and packaging revision. Mark each point as confirmed, open, not applicable or requiring specialist review, then assign an owner and due date. Evidence should identify the model and production version it covers. When a supplier answer depends on an early sample, a related product or an assumed market rule, keep the point open until the relevant production record, qualified adviser or official source supports the decision. This approach turns research into a controlled sourcing action without implying that one checklist replaces engineering, laboratory, legal, customs or transport expertise.
Good RC toy sourcing is a connected process. Product application, customer requirements, factory testing, packaging preparation and shipment inspection all need to point to the same approved configuration. The practical objective is not to add paperwork; it is to make decisions clear enough that the factory, buyer and logistics partners can act without guessing.
Use these articles alongside our RC toy product range, Shenzhen factory overview and quality-control process to turn a buying question into a project brief.
For the connected buying decisions, see RC Toy Component Shortages: Order Contingency Plan, ASTM F963 and CPSIA: RC Toy Planning Guide for U.S. Buyers, How Do I Evaluate a Supplier, MOQ, Lead Time, Quality Control, and Delivery Plan for Remote Control Toys?.
1. Define critical products and deadlines
Identify the SKUs, launch windows, materials, tools and records whose interruption creates the highest business impact.
Not every item requires the same recovery priority. Link continuity needs to retail dates, safety responsibilities and replacement-stock obligations. Share realistic demand rather than declaring every order urgent.
During factory testing and shipment preparation, use define critical products and deadlines as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
2. Map single points of failure
Review sole molds, test fixtures, trained technicians, utilities, data systems, battery sources and logistics routes.
A list of alternate factories is not enough if the mold, approved PCB or artwork cannot be transferred. Estimate which dependency limits recovery and which preventive action is proportionate before a disruption occurs.
During factory testing and shipment preparation, use map single points of failure as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Share your target market, product category and expected quantity for a focused recommendation.
3. Set incident ownership
Name who declares an incident, protects people, assesses product status and communicates with the buyer.
The first report should state known facts, affected orders, immediate containment and the next update time. Avoid optimistic dates before material, equipment and quality status are understood. A single commercial contact should coordinate technical inputs.
During factory testing and shipment preparation, use set incident ownership as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
4. Protect product and records
Define how work in process, batteries, molds, approved samples, digital files and traceability data are secured.
After a utility or building event, unseen damage or mixed status can affect output. Quarantine uncertain items and preserve records needed to decide their disposition. Backups should be tested and access rights controlled.
During factory testing and shipment preparation, use protect product and records as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
5. Qualify alternate routes
Predefine which equipment, provider or site alternatives require sample, engineering, compliance or buyer approval.
Emergency pressure does not make an unapproved substitution acceptable. Compare alternate output with the controlled baseline and repeat affected tests. Document deviations and time limits for temporary arrangements.
During factory testing and shipment preparation, use qualify alternate routes as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
6. Plan a controlled restart
Use line clearance, first-article checks, equipment verification and staged release after recovery.
A restarted line may contain mixed components or settings from interrupted work. Inspect representative units and confirm records before full volume resumes. Update inspection priorities based on the event.
During factory testing and shipment preparation, use plan a controlled restart as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
7. Review exercises and lessons
Test communication and recovery assumptions periodically and close gaps found in actual incidents.
A tabletop exercise can reveal obsolete contacts or inaccessible files without stopping production. After an event, update recovery times and preventive maintenance. Buyers should review meaningful changes at future supplier meetings.
During factory testing and shipment preparation, use review exercises and lessons as a named handoff. Record the agreed condition, identify the person who checks it, and keep the result with the project file. This does not need to become a complicated report: a controlled product specification, dated sample photos, a packing reference and a short inspection record are often enough to make customer requirements traceable. The important point is that a later sample change, production question or buyer request can be checked against a visible reference rather than memory.
Buyer check
Before moving forward, ask the supplier to show how this point is captured in the product brief, approved sample record, production preparation or shipment inspection plan. A clear answer should name the reference, the responsible person and the timing of the check. If the answer cannot be tied to an approved configuration, treat it as an open decision rather than an agreed production instruction.
Illustrative buyer scenario
A shared test station becomes unavailable during an RC car production run. Assembly continues, but finished units accumulate without the agreed function record and the shipment date becomes uncertain. In this illustrative scenario, the supplier’s continuity plan names a validated backup station, decision owner and controlled restart sample. The buyer receives a dated impact estimate and approves a revised inspection window rather than learning about the delay after the forwarder arrives.
Reference and compliance note
This article is practical buyer guidance, not legal, safety or transport advice. For the selected product and destination, verify applicable requirements with qualified laboratories, compliance advisers, carriers or authorities. For further reading, see ISO quality management guidance on external providers: Official ISO auditing guidance on controlling externally provided products and services.
Photography plan for this article
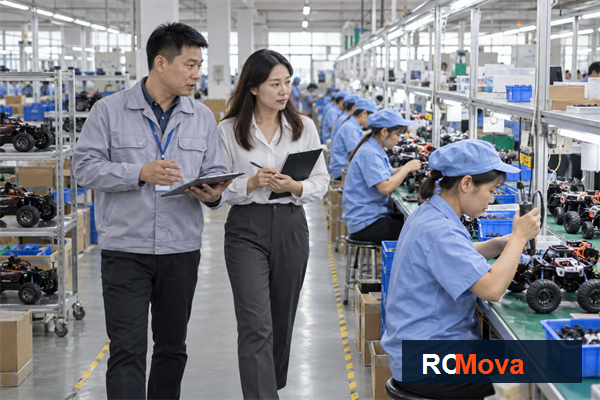
Article hero image — After the opening section
Image title: RC Toy Supplier Business Continuity Planning — RC toy sourcing overview
Caption: A factory audit is more useful when buyers follow the product flow from assembly through packing. Article focus: rc toy supplier continuity plan.
ALT text: Asian buyer and factory supervisor reviewing an RC toy production line in Shenzhen; rc toy supplier continuity plan buyer guide
Image size: 600 × 400 px
AI photography prompt: Documentary commercial photography for RC Toy Supplier Business Continuity Planning, realistic RC toy products and Shenzhen factory setting, Asian staff if people appear, natural light, authentic details, no invented certificates, no text overlays, 3:2 landscape
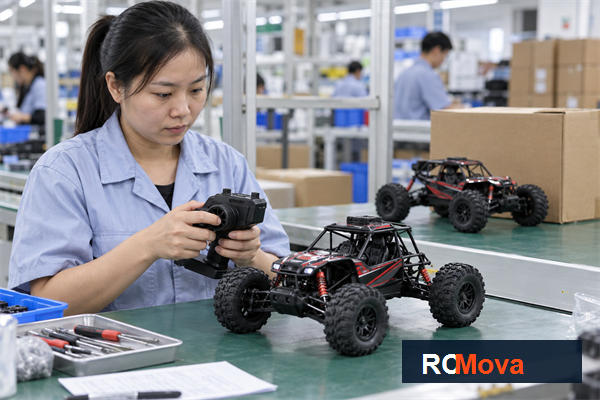
In-article supporting image — Before the FAQ section
Image title: RC Toy Supplier Business Continuity Planning — RC toy quality and shipment check
Caption: Production review for rc toy supplier continuity plan before the export handoff.
ALT text: Asian quality team reviewing rc toy supplier continuity plan with a remote control toy at the factory
Image size: 600 × 400 px
AI photography prompt: Realistic editorial photography showing a buyer checking rc toy supplier continuity plan against an RC toy sample and shipment records, Asian staff if people appear, natural industrial lighting, no text or fabricated logos, 3:2 landscape
Frequently Asked Questions
What should buyers check first about define critical products and deadlines?
Identify the SKUs, launch windows, materials, tools and records whose interruption creates the highest business impact. Not every item requires the same recovery priority. Link continuity needs to retail dates, safety responsibilities and replacement-stock obligations. Share realistic demand rather than declaring every order urgent.
How should buyers verify protect product and records?
Define how work in process, batteries, molds, approved samples, digital files and traceability data are secured. After a utility or building event, unseen damage or mixed status can affect output. Quarantine uncertain items and preserve records needed to decide their disposition. Backups should be tested and access rights controlled.
What should be confirmed before shipment?
Test communication and recovery assumptions periodically and close gaps found in actual incidents. A tabletop exercise can reveal obsolete contacts or inaccessible files without stopping production. After an event, update recovery times and preventive maintenance. Buyers should review meaningful changes at future supplier meetings.
Conclusion: turn the decision into a working plan
Identify single points of failure, define recovery priorities and evidence, and agree buyer communication and product requalification before an alternate process is used. When the selected product, sample, documentation, inspection points and shipment handoff are visible, the buying team can move with greater confidence and fewer avoidable changes.
Send Your Requirements